

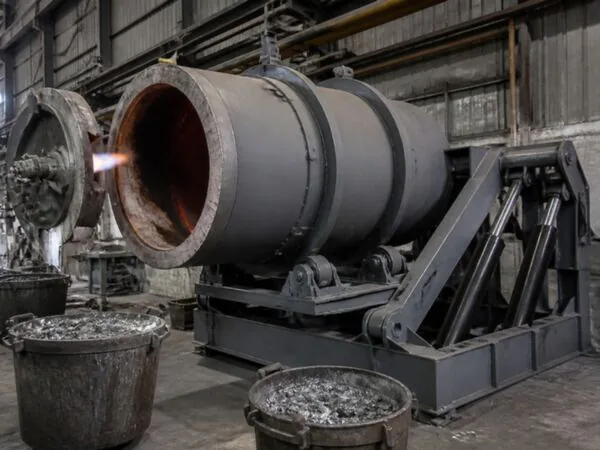
Rotary Tilting Melting Furnace
Tilting rotary furnace for dross, light scrap and mixed aluminium charges
View detailsContinuous shaft melter with holding bath for die casting and foundry lines
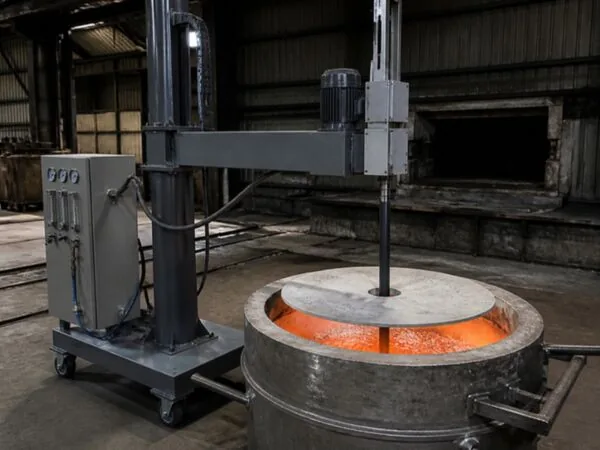
A shaft (tower) furnace where ingots and bulky returns are charged at the top and preheated by the flue gas on their way down to the melting zone, with an integrated holding bath at pouring temperature. A dross and iron inserts trap is included to avoid alloy contamination. It is used in die casting and gravity foundries that need a steady supply of liquid metal over several shifts.

With this information we can ask the right factories and come back with a proposal that fits your process. Missing something? Send what you have: we fill the gaps together.
Request a Quote Printable checklist to fill with your plant teamWe reply in English, Spanish, Italian or Chinese.
Need something different? We adapt sizes, materials and specs to your drawing.
A common rule of thumb is a holding bath in kg of at least one to two times the melt rate in kg/h. Below about 150 kg/h tapping rate, two-chamber units lose efficiency.
Shaft furnaces are designed for ingots and bulky returns. Chips and light gauge scrap are better handled in a sidewell or vortex furnace or a rotary furnace.
Tilting rotary furnace for dross, light scrap and mixed aluminium charges
View details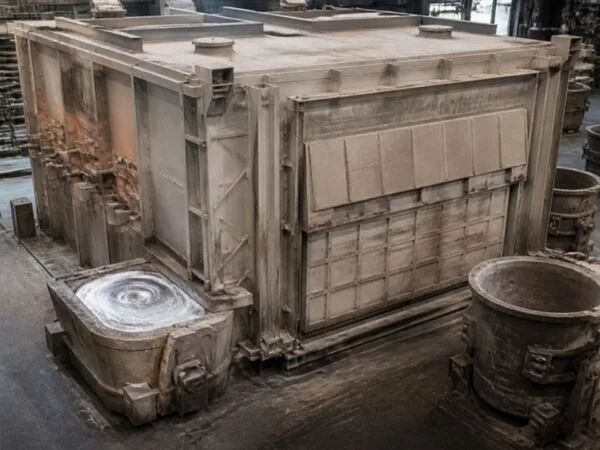
Reverberatory holding furnace with a small sidewell for returns and light scrap
View details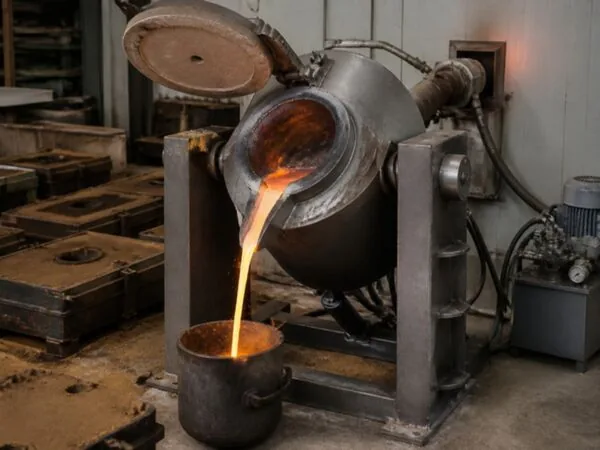
Tilting crucible furnace, fuel, gas or induction fired, for small foundries
View detailsAccessibility
No product matches that search. We source to your specification: tell us what you need.
One request, one supplier, one shipment. No prices: we quote to your spec.
Request a quote Printable RFQ sheet